Capability
CNC Milling Services from India
Looking for a reliable source of CNC Milling? Precision Machining India manufactures to your drawing at our ISO 9001:2015 certified plant in Pune, India, and supplies OEMs and procurement teams worldwide.
ISO 9001:2015 Certified
Documented quality management system
Mitutoyo Quality Inspection
Calipers, micrometers, height gauge, DTIs
Export-Ready Packaging
VCI film, ISPM-15 wooden crates
RFQ Response in 24 Hours
Quote within one working day
NDA Available
Your drawings stay confidential
On this page15 sections
Direct answer
What you get when you order CNC Milling
3-axis milled profiles, pockets, slots and flats. The work is quoted from your drawing and 3D model, made to the revision you release, and delivered with a dimensional inspection report for the batch. Standard capability for this process is ±0.02 mm general; ±0.01 mm on critical bores by agreement. Each material on the job gets its own tool geometry, speeds and inspection timing, because Aluminium and Delrin (Acetal / POM) will not hold the same limits in the same set-up. There is no fixed minimum order: a single prototype and a 10,000-piece release follow the same documented route through programming, first-article inspection and export packing from our ISO 9001:2015 certified shop in Pune.
- Tolerance: ±0.02 mm general; ±0.01 mm on critical bores by agreement
- Materials: Aluminium, Stainless Steel, Brass, Delrin (Acetal / POM), PEEK and others to drawing
- Typical parts: flanges, valve components and insulators
- Quoted within 24 hours, NDA on request, no minimum order quantity
At a glance
Materials & technical specifications
Material choice drives cost, lead time and performance. We stock or source certified bar and plate in Aluminium, Stainless Steel, Brass, Delrin (Acetal / POM) and PEEK, with EN 10204 3.1 material certificates available on request.
- Process
- CNC Milling
- Materials
- Aluminium, Stainless Steel, Brass, Delrin (Acetal / POM), PEEK, Nylon
- Standard tolerance
- ±0.02 mm general; ±0.01 mm on critical bores by agreement
- Surface finish
- As-machined, bead blast, clear or hard anodise (partner), chromate conversion
- Max turning size
- Ø400 × 1200 mm (conventional), bar work on CNC lathes
- Max milling envelope
- 800 × 500 × 400 mm (VMC)
- Threading
- M3–M32 auto tapping; metric, BSP, NPT, UNC/UNF
- Batch size
- 1 prototype to 10,000+ pieces
CNC Milling: overview
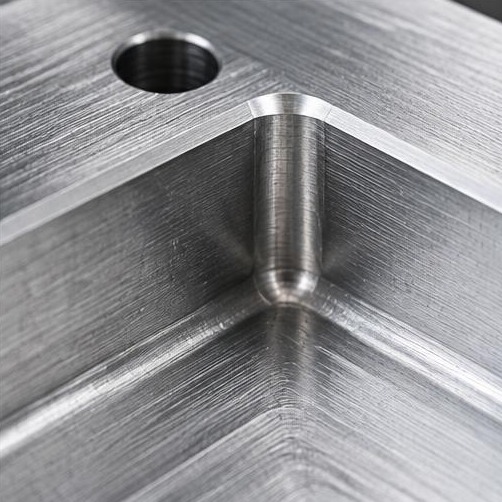
3-axis milled profiles, pockets, slots and flats. A rotating end mill removes material from a fixed workpiece along programmed toolpaths generated in VISI and Delcam CAM.
Every order is programmed in VISI or Delcam CAM, machined on Ace Micromatics VMC with FANUC control, 800 × 500 × 400 mm working envelope, and inspected in our Mitutoyo quality lab before it is packed and shipped.
CNC Milling capability
Our cnc milling cell handles single prototypes through repeat batches of tens of thousands. Typical work includes flanges, valve components and insulators.
Before quoting, our engineers review your STEP, IGES or PDF drawing for machinability and suggest changes that reduce cost without affecting function.
- CNC turning centres (LMW, Jyoti, Ace Micromatics): Shafts, bushings, fittings, turned plastic parts
- Vertical machining centre (VMC) (Ace Micromatics, FANUC control): 3-axis milling, bed 800 × 500 × 400 mm
- Auto tapping machines (M3 to M32 capacity): High-volume internal threading
- Conventional lathe (Uma Enterprises): Turning up to Ø400 × 1200 mm
- Band saw (Rajlaxmi): Bar stock cutting and blank preparation
Tolerances & surface finish
Standard capability for this work is ±0.02 mm general; ±0.01 mm on critical bores by agreement. Bores can be held to H7 and bearing seats to h6/g6 fits. Where your drawing calls for tighter limits, we agree the critical characteristics up front and record them on the inspection report.
As-machined finishes of Ra 1.6–3.2 µm suit most functional surfaces. For seals, bearing journals and sliding fits we run a fine finishing pass to reach Ra 0.8 µm.
Plating, anodising, passivation and heat treatment are arranged through qualified partners and re-inspected in-house before packing.
Quality inspection process
Our ISO 9001:2015 system covers incoming material, first-article inspection, in-process checks and final inspection. Records are kept for every batch so any part can be traced back to its material heat.
Every shipment includes a dimensional inspection report, with material test certificates (EN 10204 3.1) on request.
- Mitutoyo digital vernier calipers
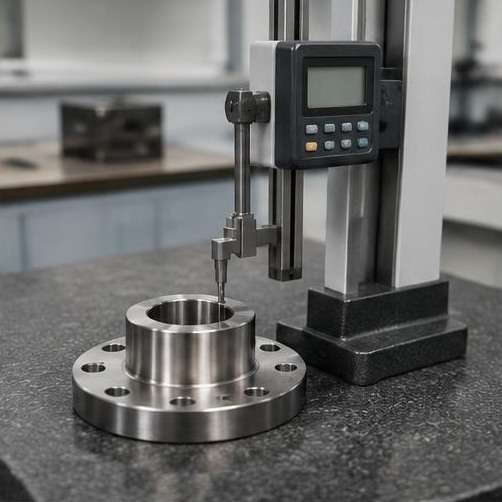
- Mitutoyo height gauge
- Granite surface plate
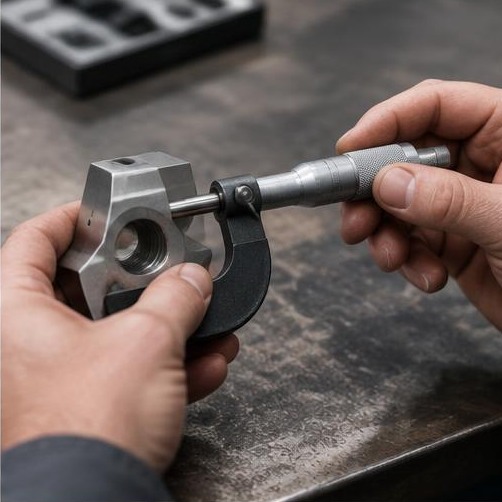
- Mitutoyo outside micrometers
- Inside calipers and bore gauges
- Dial test indicators
Envelope, tolerance and quantity
Three things decide whether a part belongs here: its size, the tightest feature on it and the quantity you need. The figures below are the limits of the machines and instruments actually in the Pune shop.
Size and set-up
Will the part fit our machines
- Turned diameter
- Up to Ø400 mm on the conventional lathe; smaller bar and billet work on the CNC turning centres
- Turned length
- Up to 1200 mm between centres
- Milled envelope
- 800 × 500 × 400 mm on the 3-axis VMC
- Threading
- M3 to M32 auto tapped; metric, BSP, NPT and UNC/UNF single-point or thread-milled
- Blanks
- Cut to length on the band saw and deburred, with the heat number carried through to the works order
Tolerance, fits and finish
What is held, and how it is checked
- Standard for this work
- ±0.02 mm general; ±0.01 mm on critical bores by agreement
- Unmarked dimensions
- ISO 2768-m unless your drawing states another class
- Fits
- ISO 286 h6, j6, k6 seats and H7 bores on metal features; clearances agreed in millimetres on polymer features
- Surface finish
- Ra 1.6–3.2 µm as machined; Ra 0.8 µm on turned bearing and sealing surfaces
- Verified with
- Mitutoyo micrometers, vernier calipers and height gauge, inside calipers, bore gauges and dial test indicators on a granite surface plate
- Measured when
- After the part has stabilised at room temperature, so the reading on the report is the one you will receive
Quantity, quote and paperwork
From RFQ to crated batch
- Batch size
- One prototype to 10,000+ pieces, with no fixed minimum order quantity
- RFQ turnaround
- A price and a lead time within 24 hours of a drawing, quantity, material and destination
- Lead time
- Quoted per batch with the price; any partner plating, anodising, passivation or heat treatment is listed as its own step
- First article
- Dimensional report on new parts for your sign-off before the balance is machined
- With every shipment
- Inspection report, commercial invoice, packing list and certificate of origin; EN 10204 3.1 material certificates on request
- Incoterms
- EXW Pune, FOB Nhava Sheva (JNPT) or Mumbai, or CIF your port
How a CNC Milling order runs
The same five stages for a one-off and for a scheduled release. Nothing is cut before the quote and the drawing revision are agreed in writing.
- 01
Drawing in, NDA first if you want one
Send the PDF with a STEP or IGES model, the grade, the batch quantity and the destination. We sign an NDA before the files move if your part is confidential.
- 02
DFM review and quotation
An engineer rebuilds the set-ups in VISI or Delcam, queries anything undimensioned or unmeasurable, and flags features that cost more than they return. Price and lead time come back within 24 hours.
- 03
Material, certificates and blanks
Bar or plate is bought to grade and cut to length on the band saw. Heat numbers are recorded against the works order, so an EN 10204 3.1 certificate can be issued for the batch later.
- 04
Programme, first-off and sign-off
The verified toolpath is loaded on the equipment this process uses — Ace Micromatics VMC with FANUC control, 800 × 500 × 400 mm working envelope — and the first part off is measured against every drawing dimension. On a new part, that report goes to you for approval before the batch continues.
- 05
Production, final inspection and packing
In-process checks run at set intervals against the agreed critical characteristics. Any partner plating, anodising, passivation or heat treatment is re-inspected here on return. Parts then go into VCI anti-rust film and ISPM-15 heat-treated crates with the full document set.
Industries we serve
This work is used across hydraulics, pumps & valves, electronics & electrical and general engineering. Hydraulics customers, for example, need leak-free sealing surfaces, accurate threads and high-pressure-rated geometry.
Our core customers are corporate OEMs in automotive, hydraulics, pumps & valves and general engineering, plus multinational companies that need PTFE, Nylon, Delrin and PEEK parts machined to drawing.
Export packaging & logistics
We export to 45+ countries from Nhava Sheva (JNPT), with sea transit of about 4–7 days to the Gulf, 18–28 days to Europe and the UK, and 25–35 days to North America. Air freight is available for urgent orders.
All parts are protected with VCI film and packed in ISPM-15 crates. We quote EXW, FOB or CIF to suit your logistics.
Why source from India with us
India has become a leading China+1 destination for precision machined components. For international buyers, we combine competitive piece prices with an ISO 9001:2015 quality system, English-speaking engineers and drawings worked to ISO, DIN and ASME standards.
We reply to RFQs within 24 hours, sign NDAs before receiving drawings, and give you one point of contact from quote to delivery.
- ISO 9001:2015 certified
- Mitutoyo quality inspection
- Export-ready packaging
- RFQ response in 24 hours
- NDA available
Drawing notes that decide the price
Most of the gap between two quotes for the same part comes from the notes around the geometry rather than the geometry itself. These are the ones that move our price the furthest.
Put this on the drawing
- Mark the three or four features that actually matter and leave the rest at ISO 2768-m. We price the recorded measurements as much as the material.
- Call fits by class rather than by a guessed deviation: H7 for a bore, h6 or k6 for a bearing seat, 6g or 6H for a thread.
- Name the datums, and say which face a runout, position or flatness call-out is measured from.
- State the grade in full — 6061-T6 and SS 303 — rather than a family name or “as per sample”.
- Put Ra values only on faces that seal, slide or locate. Everywhere else, as-machined is both cheaper and adequate.
What quietly inflates the price
- A hardness figure to be certified on the part. Heat treatment and hardness testing are done outside, so allow for the transit in the delivery date.
- Splitting an agreed batch into several small releases after the order is placed. Each release repeats the set-up and the first-off.
- A revision issued after the stock is cut. Bar is bought and sawn to the lengths on the drawing we quoted.
- Internal pocket corners below R1.5, or pockets deeper than about five times their width. Both force a long, slow cutter and extra finishing passes.
- A blanket ±0.01 mm in the title block. Every feature then earns a finishing pass and a recorded measurement, and the quote has to carry both.
How to order
Getting a quote for CNC Milling is simple:
- Send your drawing (PDF) and 3D model (STEP or IGES) with material, quantity and destination.
- Our engineers review it and send a quote with lead time within 24 hours.
- Approve samples or a first-article report for new parts.
- We machine, inspect, pack and ship with full export documents.
What is in scope, and what is not
Where CNC Milling starts and stops here, stated plainly so you can check it against your approved-vendor requirements before sending a drawing.
Programmed before anything is cut
Your model is built into set-ups in VISI or Delcam and the toolpath is simulated, so the first part off the machine is a check rather than an experiment.
Measured in-house, with the limits stated
Mitutoyo micrometers, vernier calipers and height gauge, inside calipers, bore gauges and dial test indicators, used on a granite surface plate. There is no CMM, optical comparator or hardness tester here; a feature needing one is sent out and priced that way.
The approvals we hold, and those we do not
ISO 9001:2015, with inspection records kept per batch. We do not hold AS9100 or ISO 13485 and do not take flight-critical or implanted-device work. Industrial, hydraulic, pump, valve and general engineering parts are the normal scope.
Finishing through qualified partners
Plating, anodising, passivation and heat treatment are done by qualified partners and re-inspected here before packing, so one purchase order still covers the finished part.
Traceability you can audit
Heat numbers carried from bar to works order, EN 10204 3.1 material certificates on request, a dimensional inspection report with every shipment, and an NDA signed before drawings change hands.
Packed and documented for export
VCI anti-rust film and ISPM-15 heat-treated crates, with commercial invoice, packing list, certificate of origin and inspection report. Parts leave Pune for 45+ countries EXW, FOB Nhava Sheva (JNPT) or Mumbai, or CIF.
Frequently asked questions
Get a quote in 24hWhat tolerances can you hold for CNC Milling?
Standard capability is ±0.02 mm general; ±0.01 mm on critical bores by agreement. Bores to H7 and shaft fits to h6/g6 are routine; tighter limits are agreed per drawing.
Are you ISO certified?
Yes. We are ISO 9001:2015 certified. We do not hold AS9100 or ISO 13485, but we work under customer quality plans and supply full inspection reports and material certificates.
What files do you need for a quote?
A PDF drawing with tolerances plus a STEP or IGES model is ideal. Include material, quantity, finish and destination. We reply within 24 hours.
What is your minimum order quantity?
There is no fixed MOQ. We machine single prototypes, low-volume batches and high-volume production runs.
Do you export?
Yes. We export to 45+ countries across North America, Europe, the Middle East, Africa, Asia-Pacific and Latin America.
Keep exploring
Related capabilities, materials and markets
Everything below is machined in the same Pune plant to the same ISO 9001:2015 system. Follow whichever is closest to the part you are sourcing.
Capabilities & related parts
4Export markets
8Request for quotation
Send your drawing. Get a quote in 24 hours.
Upload STEP, IGES or PDF files. NDA available on request. Quoting: CNC Milling.