Material
Nylon Machining & Custom Parts
Looking for a reliable source of nylon Machined Parts? Precision Machining India manufactures to your drawing at our ISO 9001:2015 certified plant in Pune, India, and supplies OEMs and procurement teams worldwide.
ISO 9001:2015 Certified
Documented quality management system
Mitutoyo Quality Inspection
Calipers, micrometers, height gauge, DTIs
Export-Ready Packaging
VCI film, ISPM-15 wooden crates
RFQ Response in 24 Hours
Quote within one working day
NDA Available
Your drawings stay confidential
On this page15 sections
Direct answer
Can you machine Nylon, and in which grades?
Yes. Precision Machining India machines Nylon parts to customer drawings at its ISO 9001:2015 certified plant in Pune, India, in Nylon 6, Nylon 66, cast nylon, oil-filled and MoS₂-filled. Work is turned on CNC turning centres and milled on a 3-axis VMC with a 800 × 500 × 400 mm bed, holding ±0.05 mm typical. Grades are stocked or sourced against your specification, and EN 10204 3.1 mill certificates are supplied on request. Quantities run from a single prototype to 10,000+ pieces with no fixed minimum, and RFQs are answered within 24 hours.
- Grades: Nylon 6, Nylon 66, cast nylon, oil-filled and MoS₂-filled
- Tolerance: ±0.05 mm typical
- Finishes: As-machined
- Typical parts: bushings, wear pads, rollers and pulleys
- Quantities: single prototype to 10,000+ pieces, no fixed minimum order
- Documents: dimensional inspection report with the shipment, EN 10204 3.1 mill certificate on request
At a glance
Materials & technical specifications
Nylon machining notes: Absorbs moisture, so we agree final dimensions and conditioning with you.
- Process
- Nylon Machining
- Materials
- Nylon
- Grades
- Nylon 6, Nylon 66, cast nylon, oil-filled and MoS₂-filled
- Key properties
- Tough, wear and impact resistant, self-lubricating grades available.
- Standard tolerance
- ±0.05 mm typical
- Surface finish
- As-machined
- Max turning size
- Ø400 × 1200 mm (conventional), bar work on CNC lathes
- Max milling envelope
- 800 × 500 × 400 mm (VMC)
- Threading
- M3–M32 auto tapping; metric, BSP, NPT, UNC/UNF
- Batch size
- 1 prototype to 10,000+ pieces
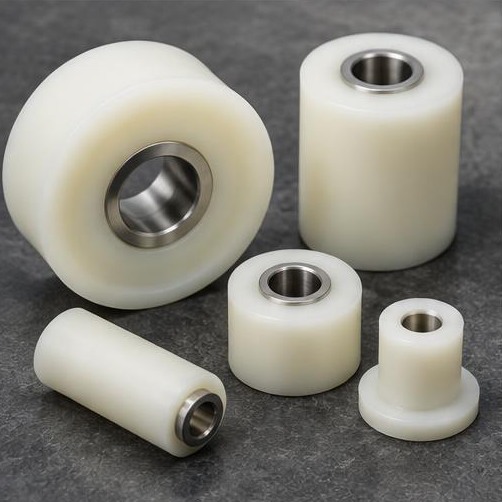
Nylon Machined Parts: overview
Wear-resistant nylon bushings, rollers and wear pads. Cast and extruded nylon is turned and milled, allowing for moisture absorption in the final dimensions agreed with you.
Every order is programmed in VISI or Delcam CAM, machined on CNC turning centres and VMC, and inspected in our Mitutoyo quality lab before it is packed and shipped.
Nylon Machining capability
We run nylon machining on dedicated machines, so prototypes, pilot lots and production runs all follow the same documented process. Common parts include bushings, insulators and seals & rings.
Before quoting, our engineers review your STEP, IGES or PDF drawing for machinability and suggest changes that reduce cost without affecting function.
- CNC turning centres (LMW, Jyoti, Ace Micromatics): Shafts, bushings, fittings, turned plastic parts
- Vertical machining centre (VMC) (Ace Micromatics, FANUC control): 3-axis milling, bed 800 × 500 × 400 mm
- Auto tapping machines (M3 to M32 capacity): High-volume internal threading
- Conventional lathe (Uma Enterprises): Turning up to Ø400 × 1200 mm
- Band saw (Rajlaxmi): Bar stock cutting and blank preparation
Tolerances & surface finish
Standard capability for this work is ±0.05 mm typical. Bores can be held to H7 and bearing seats to h6/g6 fits. Where your drawing calls for tighter limits, we agree the critical characteristics up front and record them on the inspection report.
Surface finish is typically Ra 1.6–3.2 µm as machined, with Ra 0.8 µm achievable on turned sealing and bearing surfaces. Plastics are finished with sharp tools to avoid smearing and burrs.
Plating, anodising, passivation and heat treatment are arranged through qualified partners and re-inspected in-house before packing.
Quality inspection process
Quality is built into every step under our ISO 9001:2015 management system. Raw material is checked against its mill certificate, the first article is fully inspected against the drawing, and in-process checks run at defined intervals.
Every shipment includes a dimensional inspection report, with material test certificates (EN 10204 3.1) on request.
- Mitutoyo digital vernier calipers
- Mitutoyo height gauge
- Granite surface plate
- Mitutoyo outside micrometers
- Inside calipers and bore gauges
- Dial test indicators
Nylon grades we machine
Each grade behaves differently on the machine and in service. Name the one you need on the drawing — this is what each is normally chosen for.
Nylon 6 (PA6)
Extruded
- Condition
- Extruded rod and plate
- Key property
- Tough and wear resistant; absorbs moisture, so parts grow slightly in service
- Typical use
- Bushings, wear pads and rollers in general machinery
Nylon 66 (PA66)
Extruded
- Condition
- Extruded rod and plate
- Key property
- Stiffer and harder than PA6 with a higher melting point, but more notch sensitive
- Typical use
- Gears, rollers and pulleys where stiffness matters
Cast nylon (PA6 G)
Monomer cast
- Condition
- Cast billet and large-diameter rod
- Key property
- Lower internal stress than extruded stock, so machined parts hold shape better
- Typical use
- Large bushings, sleeves, wear pads and sheaves
Oil-filled and MoS₂-filled cast nylon
Lubricated grades
- Condition
- Cast billet with the lubricant blended through the section
- Key property
- Lower friction and wear for dry running; MoS₂ grades are harder and more stable
- Typical use
- Dry-running bushings, slide pads and chain guides
Choosing between Delrin and Nylon
Delrin is the material most often quoted as an alternative to Nylon for this kind of part. The differences that change a decision are below.
| Criterion | Delrin (Acetal / POM) Stiff, stable and the best value for precision plastic parts | Nylon Tough and low cost, but it moves with moisture |
|---|---|---|
| Machinability and cycle time | The best-behaved machinable plastic: clean chips, crisp edges and tight tolerances with standard tooling, provided cutting heat is kept off the surface. | Machines well, but it takes up moisture and relieves internal stress, so final dimensions and any conditioning are agreed with you. Cast stock is more stable than extruded. |
| Tolerance we hold | ±0.02 mm typical | ±0.05 mm typical |
| Service temperature | Continuous service to about 100 °C. POM-C copes with hot water and alkaline conditions better than the homopolymer. | Continuous service around 80–100 °C. Stiffness and strength drop as the material absorbs moisture. |
| Corrosion and chemical resistance | Sound with fuels, oils, solvents and neutral chemicals. Strong acids and oxidising agents attack it, and prolonged chlorinated water is best avoided. | Good with fuels, oils, greases and alkalis. Strong acids attack it, and prolonged hot water or unprotected sunlight degrades it. |
| Relative cost | Moderate material cost and fast cycle times, which is why it is usually the cheapest route to a close-tolerance plastic part. | The lowest-cost engineering plastic we machine, and cast grades come in large diameters that keep big bushings cheap. |
Values are indicative figures from published grade data, given to guide specification rather than to qualify a design; confirm them against the mill or polymer data sheet for your service conditions. Material selection remains your design responsibility. Grades are stocked or sourced per order, with EN 10204 3.1 certificates on request.
Industries we serve
This work is used across medical devices, automotive, hydraulics and pumps & valves. Medical Devices customers, for example, need clean, burr-free parts in biocompatible materials with lot traceability.
Our core customers are corporate OEMs in automotive, hydraulics, pumps & valves and general engineering, plus multinational companies that need PTFE, Nylon, Delrin and PEEK parts machined to drawing.
Export packaging & logistics
We export to 45+ countries from Nhava Sheva (JNPT), with sea transit of about 4–7 days to the Gulf, 18–28 days to Europe and the UK, and 25–35 days to North America. Air freight is available for urgent orders.
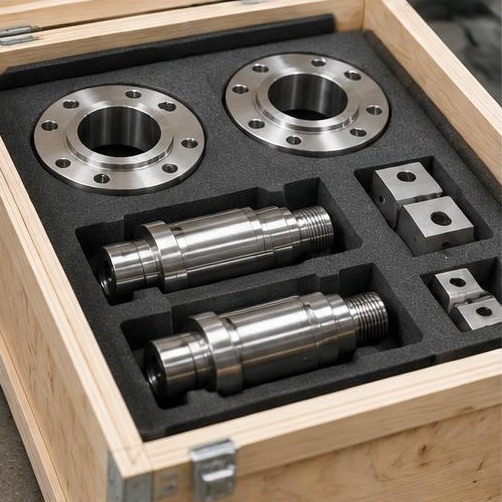
All parts are protected with VCI film and packed in ISPM-15 crates. We quote EXW, FOB or CIF to suit your logistics.
Why choose an Indian machining partner
India has become a leading China+1 destination for precision machined components. For international buyers, we combine competitive piece prices with an ISO 9001:2015 quality system, English-speaking engineers and drawings worked to ISO, DIN and ASME standards.
You get a 24-hour RFQ response, an NDA on request, one engineer as your contact, and inspection reports with every shipment.
- ISO 9001:2015 certified
- Mitutoyo quality inspection
- Export-ready packaging
- RFQ response in 24 hours
- NDA available
Specifying Nylon on your drawing
A drawing that answers these points can be quoted in one pass and machined without a query.
Put this on the drawing
- Name the polymer and the filler — Nylon 6 (PA6), for example — because filled and unfilled grades cut and move differently.
- Give the service temperature, the chemicals in contact and the mating material, so the grade can be confirmed against the maker's data sheet.
- Ask for the tolerance you actually need: ±0.05 mm typical is standard, and tighter limits mean extra passes and stress relieving.
- State whether dimensions apply as machined or after conditioning at a stated temperature and humidity.
- Keep wall thicknesses sensible and corners radiused so parts do not deflect under clamping.
- Ask for individual bagging; machined plastics scratch and pick up contamination in bulk packing.
What causes scrap, delay or extra cost
- Metal tolerances on a polymer: a few degrees of temperature change moves a 100 mm plastic part more than ±0.01 mm.
- Thin unsupported walls and deep narrow slots, which deflect away from the tool and spring back after the cut.
- Press fits into metal with no allowance for the difference in thermal expansion across the working temperature range.
- Acceptance measured straight off the machine; parts must stabilise at a known temperature first.
- Biocompatibility or implant approval. The certification held is ISO 9001:2015, not ISO 13485; what is supplied is the material maker's data sheet and batch documentation.
- Reports from a CMM or in-house material testing — neither exists here; dimensional checks are made with Mitutoyo hand instruments on a granite surface plate.
How to order
Getting a quote for nylon Machined Parts is simple:
- Send your drawing (PDF) and 3D model (STEP or IGES) with material, quantity and destination.
- Our engineers review it and send a quote with lead time within 24 hours.
- Approve samples or a first-article report for new parts.
- We machine, inspect, pack and ship with full export documents.
What to weigh when buying Nylon parts
Properties quoted here are those of the material as supplied. Pressure ratings and application approval stay with your own design and qualification process.
Service temperature
Continuous service around 80–100 °C. Stiffness and strength drop as the material absorbs moisture.
Dimensional stability
Machines well, but it takes up moisture and relieves internal stress, so final dimensions and any conditioning are agreed with you. Cast stock is more stable than extruded. Parts are measured after they have stabilised in temperature, not straight off the machine.
Chemical compatibility
Good with fuels, oils, greases and alkalis. Strong acids attack it, and prolonged hot water or unprotected sunlight degrades it.
Tolerance and fit
Standard capability on Nylon is ±0.05 mm typical. Closer limits are possible on selected diameters when the stock is stress-relieved and the finishing pass is light.
Electrical properties
Unfilled and glass-filled grades are insulators; carbon- and metal-filled grades conduct, so state on the drawing if the part has to isolate.
Handling and packing
As-machined. Parts are bagged to keep sealing and sliding faces free of scratches and metallic contamination, then crated in ISPM-15 heat-treated timber.
Frequently asked questions
Get a quote in 24hWhat tolerances can you hold for nylon Machined Parts?
Standard capability is ±0.05 mm typical. Bores to H7 and shaft fits to h6/g6 are routine; tighter limits are agreed per drawing.
Are you ISO certified?
Yes. We are ISO 9001:2015 certified. We do not hold AS9100 or ISO 13485, but we work under customer quality plans and supply full inspection reports and material certificates.
What files do you need for a quote?
A PDF drawing with tolerances plus a STEP or IGES model is ideal. Include material, quantity, finish and destination. We reply within 24 hours.
What is your minimum order quantity?
There is no fixed MOQ. We machine single prototypes, low-volume batches and high-volume production runs.
Do you export?
Yes. We export to 45+ countries across North America, Europe, the Middle East, Africa, Asia-Pacific and Latin America.
Which Nylon grades do you machine?
Nylon 6, Nylon 66, cast nylon, oil-filled and MoS₂-filled. Other grades on request.
Keep exploring
Related capabilities, materials and markets
Everything below is machined in the same Pune plant to the same ISO 9001:2015 system. Follow whichever is closest to the part you are sourcing.
Request for quotation
Send your drawing. Get a quote in 24 hours.
Upload STEP, IGES or PDF files. NDA available on request. Quoting: Nylon Machined Parts.